“`html
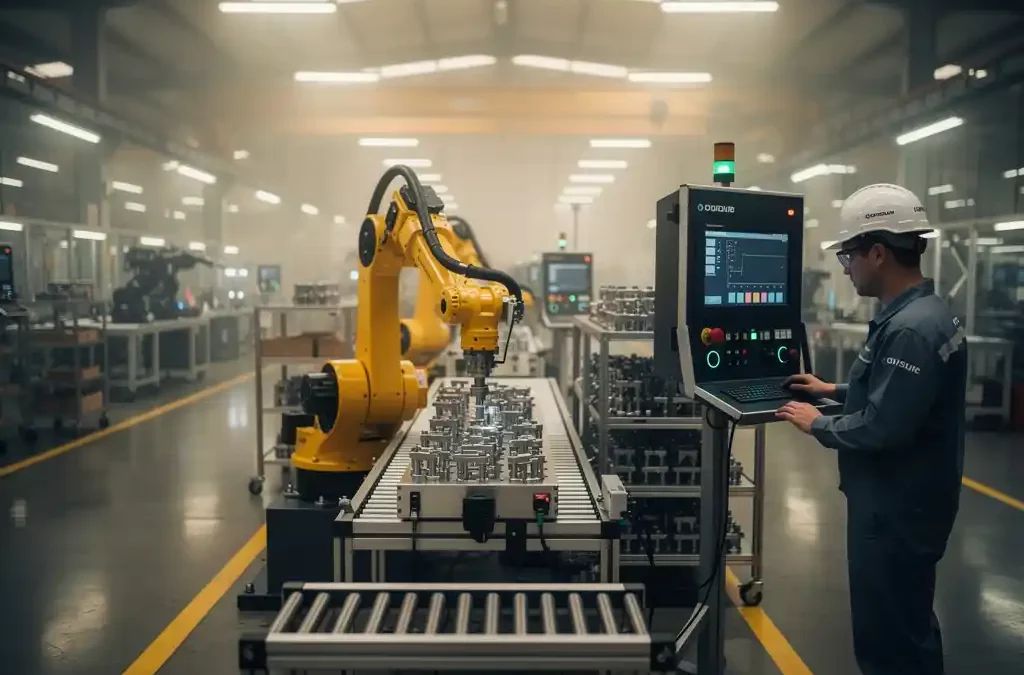
A well-run factory is characterized by streamlined operations, real-time data accessibility, and consistent quality control. These factories integrate technology to enhance production efficiency and optimize processes, allowing for the quick identification and resolution of issues. By focusing on data-driven decisions and continuous improvement, they ensure maximum production capacity utilization and minimize production loss. In this article, we’ll explore how technology aids factory operations, the benefits of a digital shopfloor, and how to overcome challenges in digital transformation.
What defines a well-run factory?
A well-run factory is defined by its ability to maintain efficient production processes, ensure high-quality outputs, and make informed decisions based on real-time data. This includes having standardized procedures, effective communication systems, and integrated technology solutions that enhance production performance and minimize downtime.
In such factories, every aspect of the operation, from inventory management to quality control, is optimized to reduce waste and improve productivity. Real-time visibility into production status allows managers to address issues promptly, ensuring that production loss is minimized. Additionally, these factories often employ continuous improvement practices, such as lean management, to sustain operational excellence.
How does technology improve factory operations?
Technology improves factory operations by providing tools for automation, data analysis, and process optimization. It enables factories to monitor production in real time, identify inefficiencies, and implement solutions swiftly. This leads to enhanced production efficiency and reduced production loss.
For instance, digital work instructions ensure that operators follow standardized procedures, reducing variability in production. Real-time dashboards provide insights into machine performance and production capacity utilization, allowing for proactive management. Moreover, technologies like AI and IoT facilitate predictive maintenance, preventing unexpected downtime and extending equipment lifespan.
What are the benefits of a digital shopfloor?
A digital shopfloor offers numerous benefits, including improved production efficiency, enhanced data accuracy, and streamlined communication. By digitizing operations, factories can reduce manual errors, increase transparency, and optimize resource allocation.
With a digital shopfloor, data is collected and analyzed continuously, providing actionable insights that drive decision-making. This enables factories to respond quickly to changes in demand or production issues, ultimately leading to better production performance. Additionally, digital systems facilitate collaboration across departments, ensuring that everyone is aligned and informed.
How can factories achieve operational excellence?
Factories can achieve operational excellence by implementing standardized processes, leveraging technology for real-time insights, and fostering a culture of continuous improvement. This involves setting clear performance metrics, regularly reviewing processes, and encouraging innovation.
Operational excellence is also achieved by integrating systems that connect the shopfloor with management, ensuring seamless communication and data flow. By adopting lean manufacturing principles and focusing on reducing production loss, factories can enhance their overall efficiency and competitiveness.
What challenges do factories face in digital transformation?
Factories face several challenges in digital transformation, including resistance to change, integration with existing systems, and ensuring data security. These challenges can hinder the adoption of new technologies and delay the realization of benefits.
To overcome these obstacles, factories need to engage stakeholders early in the process, provide adequate training, and choose scalable solutions that align with their specific needs. Additionally, addressing concerns about data privacy and ensuring robust cybersecurity measures are crucial for successful digital transformation.
How does Factorise support factories in digitalization?
Factorise supports factories in digitalization by offering a composable digital shopfloor platform that connects people, machines, and processes in real time. This platform helps manufacturers digitalize their production operations suite by suite, enhancing production efficiency without disrupting existing workflows.
Our platform integrates seamlessly with existing systems, providing real-time insights and facilitating data-driven decision-making. With modules designed for various aspects of manufacturing, Factorise allows factories to start with the most pressing issues and expand as needed. Learn more about our digital manufacturing solutions.
Ready to take the first step? We like to start with a fit-gap session: a day or two to understand where you are, which pain points are most urgent, and which modules deliver the fastest value. Book your first fit-gap session. No sales pitch. Just an honest conversation about what’s realistic.
“`
Related Articles
- Why do traditional MES projects fail?
- What is OPC UA and how does it connect machines to a MES?
- What is downtime tracking and why does it matter?
- How do you double production output in three years with the same workforce?
- What is the role of data in improving manufacturing performance?
- What is lean manufacturing and how does it work?
- How do you justify a MES to a board or CFO?
- How do you build a maintenance plan for manufacturing equipment?
- How do sensors reduce machine downtime in a factory?
- How do you move from reactive to preventive maintenance in a factory?
- How do you prevent equipment breakdowns in manufacturing?
- What is reactive maintenance and why is it a problem?
- What is the difference between OEE and TEEP?
- What is the difference between a reactive and a proactive manufacturing operation?
- Why is the OEE number in most factories inaccurate?